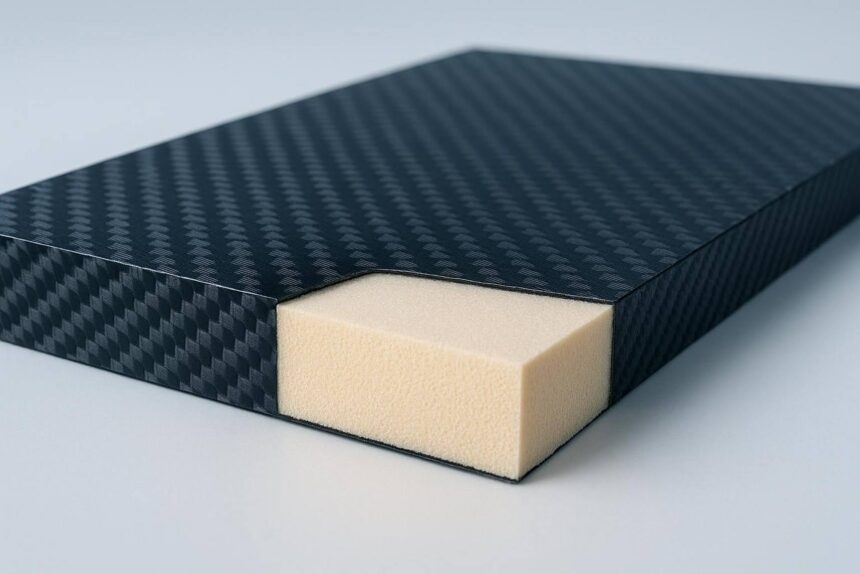
A specialized distributor supports Rohacell RIMA foam projects by connecting material supply, engineering advice, and production support. The distributor turns the technical properties of polymethacrylimide (PMI) core foam into practical manufacturing steps. Rather than acting as a simple seller, an experienced distributor helps select the right grade, reduces long factory lead times through regional stock, and supplies close-tolerance, machined core kits that fit directly into composite production lines.
Structural cores form the mechanical base of high-performance sandwich composites, so an expert supply partner can help prevent expensive scrap and processing problems. Whether the project involves advanced aircraft surfaces, automotive crash modules, or high-frequency communications equipment, sourcing Rohacell RIMA foam – distributor Chem-Craft gives fabricators genuine, certified material along with process knowledge for resin infusion, prepreg bonding, and autoclave curing.
How a Specialized Distributor Supports Rohacell RIMA Foam Projects
What Project Support Can a Rohacell Rima Distributor Provide?
Specialized distributors offer technical help through every stage of a composite program, starting before the first purchase order. They work with design engineers to review laminate schedules, calculate core shear needs, and check whether the planned process fits Rohacell RIMA’s heat and mechanical limits. This early review helps prevent poor matches between resin cure behavior and core strength.
Distributors also provide direct help with production. This may include guidance on machining settings, recommended thermoforming temperatures, and prepared near-net-shape kits with edge chamfers, cut-outs, and bonding grooves. Sending ready-to-mold core kits to the production floor simplifies the work and reduces the waste often created by cutting foam in-house.
How Technical Advice Reduces Material Selection and Processing Risks
Choosing the wrong foam density or process grade can cause part failure during high-temperature consolidation. PMI foams react to pressure differently from crosslinked PVC and honeycomb cores. Without proper process planning, the core may crush, its cell walls may collapse, or the bond between the skin and core may be weak. Technical specialists guide fabricators through pressure ramp settings and help prevent excessive heat buildup in thick laminates.
Distributors also help manage resin flow. Rohacell RIMA is made to limit resin entry into the core, but a poor vacuum infusion setup or a resin with the wrong viscosity can still create resin-rich areas, dry sections, or surface print-through. Distributors use process experience with epoxies, vinyl esters, cyanate esters, and other resin systems to set a suitable processing window and support repeatable results.
How Distributors Coordinate Samples, Quotations, and Production Orders
Buying raw PMI foam blocks directly from the chemical manufacturer often means meeting high minimum order quantities (MOQs) and waiting several months. This can delay prototype work. A dedicated distributor helps by keeping sample stock on hand. The distributor can provide small test coupons, mechanical test panels, and prototype sheets quickly. Engineering teams can then run coupon tests and resin compatibility checks without placing a full factory order.
After testing is complete, distributors can increase supply for serial production. They prepare staged quotations, account for changes in raw material prices and currency values, and set volume-based pricing. Forward blanket orders linked to production plans help maintain regular material supply and protect tier-1 and tier-2 manufacturers from delays at the factory level.
Why Local Inventory and Application Knowledge Improve Project Timelines
PMI foam is made in specialized, high-cost production plants. Lead times for raw master blocks can last several months. Specialized distributors act as regional supply buffers by storing common densities and thicknesses in warehouses across Europe, the Americas, and Asia. Local stock can turn a long factory wait into a much faster delivery.
Local application knowledge also makes technical advice more useful for each production site and its local rules. An experienced distributor understands regional aerospace and automotive OEM specifications, local humidity conditions that affect open-shop work, and the details of nearby supply chains. This local presence can support on-site engineering visits and quick fault diagnosis, helping production stay on schedule.
What Is Rohacell RIMA Foam and Why Does Grade Selection Matter?
Rohacell RIMA 51, 71, and 110: Density and Performance Differences
Rohacell RIMA, which stands for Resin Infusion Minimum Absorption, is a rigid, closed-cell foam core made from polymethacrylimide (PMI). Evonik produces the material in three main nominal densities: 51 RIMA, 71 RIMA, and 110 RIMA. Rohacell 51 RIMA has a nominal density of 52 kg/m³ (3.25 lbs/ft³). It offers a compressive strength of 0.8 MPa (116 psi), a tensile strength of 1.6 MPa (232 psi), and an elastic modulus of 75 MPa (10,878 psi). This grade suits large structures where low weight is a main requirement.
For more demanding structural parts, 71 RIMA has a density of 75 kg/m³ (4.68 lbs/ft³). Its compressive strength is 1.7 MPa (247 psi), tensile strength is 2.2 MPa (319 psi), and elastic modulus is 105 MPa (15,229 psi). At the high-strength end, 110 RIMA has a density of 110 kg/m³ (6.87 lbs/ft³). It provides a compressive strength of 3.6 MPa (522 psi), a tensile strength of 3.7 MPa (537 psi), and an elastic modulus of 180 MPa (26,107 psi). All three grades have a strain at break of 7%, supporting reliable performance under both steady and changing loads.
How Density Affects Weight, Compressive Strength, and Structural Efficiency
Choosing a density means balancing low weight with the strength needed for the part. In a sandwich composite, the core carries transverse shear loads and helps keep the face sheets stable against local buckling and wrinkling. A core with too little density may lead to face-sheet crimping or early core shear failure. A core with too much density adds weight without providing a useful structural benefit.
Higher-density grades provide much greater resistance to compression through the thickness. This matters for parts exposed to point loads, mechanical fasteners, or high tool pressure during autoclave curing. Moving from 51 RIMA to 110 RIMA increases compressive strength more than four times, from 0.8 MPa to 3.6 MPa, while the foam weight is only about twice as high. This may allow designers to remove some face-sheet plies while gaining better local impact resistance and core support.
When Rohacell RIMA Is Preferable To Other Rohacell Grades
Evonik produces several Rohacell grades for different engineering uses. These include IG/IG-F for general industrial and marine work, HERO for aerospace autoclave parts that need high damage tolerance, and XT for high-temperature thermoforming. Rohacell RIMA is different because its very fine closed-cell structure is made for liquid composite molding (LCM), including vacuum-assisted resin infusion (VARI) and resin transfer molding (RTM).
Standard foams with larger cells and traditional crosslinked foams can allow a large amount of resin to enter cut cells at the surface during infusion. This adds weight without adding structural value. Rohacell RIMA keeps this extra resin to a low level. It is often selected instead of basic grades such as Rohacell A or IG-F when the structure must be very light and production uses low-viscosity liquid resin under vacuum or pump pressure.
Which Rohacell RIMA Properties Should a Distributor Help You Evaluate?
Density, Compressive Strength, and Tensile Strength
When reviewing a design, distributors help engineers compare density, compressive strength, and tensile limits. During curing, the core must withstand inward pressure from the consolidation process without cell failure. A distributor reviews both nominal and minimum material values to confirm that the selected core keeps its shape across the planned heat and pressure range.
Tensile strength also matters because loads through the thickness can pull the core apart when the laminate skins flex under changing loads. Rohacell 51 RIMA, 71 RIMA, and 110 RIMA have tensile strengths of 1.6 MPa, 2.2 MPa, and 3.7 MPa. A distributor checks that peel and flatwise tensile loads at the bond line stay safely below the foam’s elastic limits, helping protect against skin separation in demanding service.
Shear Strength, Elastic Modulus, and Shear Modulus
For sandwich structures, bending stiffness depends heavily on core shear strength and shear modulus. A core with too little shear modulus allows excessive deflection under transverse loads and places more bending stress on the thin face sheets. Distributors compare these values with beam-deflection calculations. 51 RIMA has a shear strength of 0.8 MPa and a shear modulus of 24 MPa. 71 RIMA provides a shear strength of 1.3 MPa and a shear modulus of 42 MPa. 110 RIMA provides a shear strength of 2.4 MPa and a shear modulus of 70 MPa.
Along with elastic modulus values from 75 MPa to 180 MPa, these properties give Rohacell RIMA sandwich structures good fatigue life and stiffness under changing loads. Distributors help fabricators compare the data with other core materials. This can show where a thinner, lighter PMI section can replace a thicker, heavier material while preserving the required moment of inertia and bending stiffness.
Minimal Resin Uptake and Closed-Cell Performance
Low resin uptake is a key feature of Rohacell RIMA. Its fine, fully closed-cell structure prevents liquid resin from moving into the inner foam. Resin can wet only the small cells exposed at the cut surface. Rohacell RIMA limits resin uptake to about 50 g/m², which is very low compared with many other structural cores.
In large infusion parts such as radar housings, high-end automotive chassis tubs, wind foils, and marine foils, low resin absorption prevents kilograms of extra weight from being added to the laminate. Distributors help process engineers include the known surface resin use in infusion flow models and total resin calculations. This helps the finished part stay within its planned weight.
Heat Resistance, Creep Compression Strength, and Dimensional Stability
Standard Rohacell RIMA foam can be processed at pressures up to 0.7 MPa and temperatures up to 130°C. For hotter cycles, distributors can supply Rohacell RIMA-HT, a heat-treated version that can withstand curing temperatures up to 180°C at 0.7 MPa without major creep or cell collapse. This makes RIMA-HT suitable for aerospace hot-melt prepregs and epoxy infusion systems.
Resistance to compression creep helps the core keep its thickness during long curing cycles. If the core slowly compresses under heat and pressure, the sandwich panel can lose its correct dimensions. This may create assembly gaps and uneven skin thickness. Distributors review curing charts, including heating rates, hold times, and pressure curves, to check that the foam will retain its shape.
How Does a Distributor Match Rohacell RIMA to the Manufacturing Process?
Compatibility With Prepreg, Resin Infusion, RTM, and Autoclave Processing
Distributors such as Chem-Craft review the equipment available at the production site and recommend how Rohacell RIMA should be used with the chosen process. During vacuum infusion (VARI) and Resin Transfer Molding (RTM), the fine cell structure of RIMA limits resin bleeding into the core. This helps reduce uneven flow, race-tracking, and dry areas. The closed-cell structure also makes resin movement across the infusion area more predictable.
In autoclave prepreg work and compression molding, the core must keep its shape under high external pressure. Distributors help fabricators choose between standard RIMA and RIMA-HT. The selected grade must handle vacuum, autoclave pressure, and high temperature at the same time. This helps prevent distortion and core crushing near edge chamfers.
How Curing Temperature and Pressure Affect Core Performance
Core behavior during curing depends on the combined effects of temperature and pressure. As the temperature approaches the glass transition range, the PMI cell walls become softer. If pressure is applied too early, before the foam has reached the right structural condition, the material may compress permanently. This can change part thickness and affect the planned fiber-volume fraction.
Distributors guide process engineers in setting hold times and adjusting autoclave or press ramps. By applying consolidation pressure at the right point, often near the lowest viscosity of the resin, fabricators can achieve good laminate consolidation while keeping the inner structure of the Rohacell RIMA core intact.
Thermoforming RIMA Foam for Complex Shapes
Rohacell RIMA is a rigid thermoset PMI foam, but controlled heat and mechanical pressure allow it to form into detailed three-dimensional shapes. The foam softens within a set temperature range, usually from 165°C to 205°C. It can then be shaped over single-sided or matched tools without cracking, tearing cells, or creating wrinkles.
Distributors provide heat-processing instructions for thermoforming. They advise on oven hold times so heat reaches the center of the core, press closing speeds that reduce the chance of brittle breaks, and clamping methods that hold the part while it cools below its glass transition temperature. This allows manufacturers to make smooth, curved sandwich parts without building the core from many separate pieces.
Machining Foam Cores While Protecting Dimensional Accuracy
Rohacell PMI foams can be machined with common CNC methods, including high-speed milling, turning, drilling, and horizontal slicing. Close dimensions require the right cutter, tool shape, cutting speed, feed rate, and dust control. A fast cutter can heat or damage unsupported foam edges if the feed and spindle speeds are not balanced.
Distributors can supply machined core parts made directly from customer CAD files, with tolerances as close as ±0.1 mm or ±0.2 mm. With high-speed milling tools and vacuum tables, they can produce chamfers, pockets, step joints, and three-dimensional surfaces. Accurate machining helps the core fit the mold correctly and reduces resin pooling along edges and gaps during liquid molding.
How Drying and Heat Treatment Improve Creep Behavior
Rohacell is a closed-cell polymer, so it takes in moisture slowly through surface diffusion. If a damp core is suddenly heated above 100°C during curing, the water can turn into steam. The resulting pressure inside the material can reduce compressive strength and cause local blisters, cell collapse, or skin separation.
To reduce this risk, specialized distributors advise on conditioning procedures or carry them out in-house. For processing above 100°C, the foam is dried in a circulating-air oven at 135°C for at least 4 hours. For better creep resistance during demanding 180°C cures, the foam may receive extended heat treatment at 150°C to 180°C for as long as 48 hours. The distributor can provide the conditioned core before it reaches the production line, reducing the chance of heat-related defects.
How Does a Specialized Distributor Manage Rohacell RIMA Supply?
Rohacell RIMA Sales Ranges in Millimeters
Distributors keep Rohacell RIMA in standard industrial sheet sizes that help reduce cutting waste for common composite panel layouts. Available sheet sizes and production thicknesses depend on the selected density.
Rohacell 51 RIMA is supplied in standard sheets measuring 2500 x 1250 mm, with thicknesses from 5 mm to 80 mm. Rohacell 71 RIMA is also supplied in 2500 x 1250 mm sheets, with thicknesses from 5 mm to 65 mm. The higher-density 110 RIMA grade is supplied in 2160 x 1100 mm sheets, with thicknesses from 5 mm to 60 mm. Distributors keep a working mix of these sizes for both small subassemblies and large continuous structural skins.
Cut-To-Size Formats, Tolerances, and Machining Allowances
Most composite structures do not use raw, uncut foam blocks directly from the package. Specialized distributors fill this gap with horizontal slicing and cutting services. They can slice master blocks into custom sheets from 1 mm to 140 mm thick. Standard factory thickness tolerances of ±0.2 mm may be reduced to ±0.1 mm on request, which supports aerospace and other high-precision assemblies.
Along with flat sheets, distributors can include machining allowances for tool shapes and small changes after infusion. Core parts may arrive with edge chamfers, recesses for hard points, and relief cuts for tight radii. This reduces manual trimming on the shop floor, cuts production time, and gives each tool cycle a more consistent fit.
Sample Quantities, Minimum Orders, and Repeat Production Supply
A specialized distributor can support both early development and large-volume production. Research groups, university laboratories, and tier-1 development teams often need only a few sheets for initial coupon work. Distributors can divide master crates into single sheets or sample kits, avoiding the high MOQs that may apply to direct factory orders.
When a program reaches serial production, the distributor becomes a regular supply partner. They can set up safety stock agreements, track planned usage, and arrange scheduled batch deliveries. This gives the customer a steady supply of certified foam without requiring a large and costly stockpile at the factory.
Packaging, Storage, Moisture Control, and Delivery Planning
PMI foam quality depends on careful storage and handling, especially for pre-dried and heat-treated grades. Heat-treated versions such as Rohacell RIMA-HT are shipped in sealed, moisture-resistant aluminum barrier packaging. This limits moisture pickup during transport and storage. Specialized distributors check and protect these seals while the material is in their warehouses and during final shipping.
Distributors also arrange shipping methods that protect thin and fragile sheets from physical damage. Custom wooden crates, internal foam edge supports, and controlled storage conditions help the material arrive flat, clean, dry, and ready for lay-up. This reduces cracks caused by handling and keeps dirt away from the core surface.
How Do Quality, Approvals, and Safety Affect a RIMA Foam Project?
Material Certificates, Traceability, and Batch Documentation
Aerospace, defense, and high-end automotive programs require a clear record of material origin and production history. Specialized distributors provide batch documents with each shipment. These may include EN 10204 3.1 inspection certificates, physical property test records, and Certificates of Conformity (CoC) that confirm the material’s source and quality.
This record connects each sliced sheet and machined core to Evonik’s German production reactors and the original production lot. By handling the paperwork, distributors help customers complete quality audits and track material across production programs that may run for many years.
Aerospace Quality Management and Customer Approval Requirements
Rohacell foam has been used in high-performance structures for about 50 years, with its first aerospace specifications written in 1972. The material is supported by global aerospace quality systems certified to EN 9100:2018 / AS9100:2016. It has also been listed in the Online Aerospace Supplier Information System (OASIS) database since March 2007.
Specialized distributors align their handling, cutting, and kitting work with these aerospace quality requirements. Their quality procedures can match the approved supplier lists (ASLs) used by aerospace customers. This helps machined cores, joined blocks, and packaged kits enter flight-hardware assembly without repeated incoming inspections.
Physiological, Toxicological, and Workplace Safety Information
Rohacell RIMA is an inert, solid, crosslinked polymer with a high molecular weight. It does not dissolve in water and is generally non-toxic and physiologically inert during normal handling. The material is not absorbed through the skin, respiratory tract, or digestive system under normal conditions. It contains no CFCs and does not release ozone-depleting substances during storage at room temperature.
Distributors also give safety guidance for secondary operations. Machining and sanding produce fine dust, so local exhaust ventilation and basic personal protective equipment (PPE) are needed to reduce mechanical irritation to the airways. Fabricators should not use hot-wire cutting on Rohacell. Heat damages the PMI polymer and can release harmful fumes. Mechanical methods such as band sawing, routing, and waterjet cutting are recommended instead.
Environmental Compatibility, Waste Handling, and Recycling Options
Rohacell RIMA has a crosslinked thermoset polymethacrylimide structure, so it cannot be melted and reused like a basic thermoplastic. Its chemical makeup does allow clean thermal treatment with energy recovery. In modern industrial waste combustion plants, the foam breaks down with little ash and without releasing harmful halogenated emissions.
Distributors help composite manufacturers reduce waste by planning CNC nesting layouts carefully and limiting dry edge trim. As the composite industry works on better life-cycle performance and reuse, distributors also work with testing facilities on new end-of-life options. These include using reground PMI machining dust as an energy-saving filler in syntactic foams or casting resins. This approach, combined with accurate material planning and reuse of grades across fields such as electric vertical takeoff and landing (eVTOL) aircraft, thin-sheet acoustic diaphragms, and 5G dielectric radomes, helps Rohacell RIMA projects reduce waste while maintaining low weight and efficient production.