Thirty seconds doesn’t sound like much. Then you count how many times your wrappers stop in a shift.
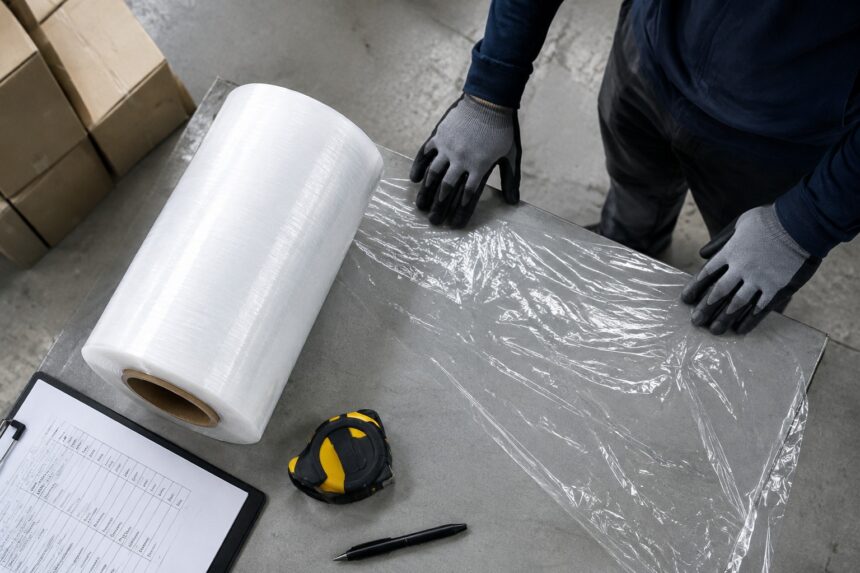
On a busy packing line, a short hand roll runs out at the worst moment: mid-pallet, with a truck waiting at the dock — a loader leaning on the door frame. The wrapper walks off, grabs a new core, fumbles the film tail, and starts over. Do that 15 or 20 times a day across a few stations and the lost minutes pile up fast (they just never show on the labor report). A plastic wrap big roll changes that math. Fewer swaps, fewer restarts, and fewer loads that get rushed at the end of the shift.
But bigger isn’t automatically better. Gauge, core size, and film consistency decide whether a machine-size roll saves you time or just jams the carriage. Here’s what 22 years on the floor teaches you about getting it right.
The roll change problem nobody puts on the labor report
Take a wrapper on second shift at a mid-size distribution center. She runs 14-inch hand rolls, and by 7 p.m. she’s swapped cores nine times. Nobody wrote it down. Nobody ever does.
That’s the gap. A plastic wrap big roll loads on a machine or a cart and keeps running, while a short hand roll runs dry mid-pallet and stops the whole line.
What a 30-second swap costs over a full shift
Thirty seconds sounds like nothing. Multiply it out. Twelve swaps a shift is six minutes, and across 10 wrappers and 250 working days, that’s 250 hours a year spent staring at an empty core. (Walking to the supply rack adds more than most people admit.)
- Dead time: the pallet sits half-wrapped, and the dock backs up.
- Tail waste: partial rolls get tossed instead of finished.
- Loose starts: every new roll begins with a weak first wrap.
Why short hand rolls force more stops than most managers count
Hand rolls are light for a reason. They’re sized for one person to carry. But an 80-gauge hand roll on a heavy pallet can run out in two or three loads. A jumbo machine roll holds many times that, so you’re stopping once a shift, not once an hour.
Count your swaps for one week. The number will surprise you.
Machine-size stretch wrap: gauge, stretch ratio, and what a big roll actually gives you
Gauge is the first spec that matters. A plastic wrap big roll built for a machine isn’t the same animal as a handheld roll from the moving aisle, and mixing them up costs you loads on the dock.
Reading gauge and core specs before you order a case
Most machine rolls run 60 to 90 gauge, and the standard width is 20 inches (some lines take 30). Check the core, too. A 3-inch core that doesn’t fit your carriage arm will sit in the box while the line sits idle. Here’s what to confirm before any case order:
- Gauge: 63 to 80 for typical mixed pallets, heavier for sharp or uneven loads
- Roll weight: 40 to 80 lbs, which is a real lift for your crew
- Core size and width: match the machine, not the catalog photo
Consistency counts. Film that swings a few gauge points from case to case gives you random tears.
Pre-stretch, film yield, and wraps per pallet
Pre-stretch is where the savings live. A 250% pre-stretch machine pulls film to 3.5 times its original length before it touches the load. Hand wrap barely hits 50%. That’s why one machine roll can cover 40 or more pallets while a handheld roll gives out after five or six.
Fewer roll changes. Fewer wraps. Less time per pallet.
Run a simple test: count wraps on your last ten pallets, then compare film used per load. If the number jumps around, the film or the settings need attention.
Heavy-duty stretch wrap for shipping: load stability and film quality
Why does a pallet that looked tight at the dock show up leaning on the other end? Usually the film, not the wrapper. A plastic wrap big roll only saves time if every foot of it behaves the same way.
Machine rolls run fast. Bad film runs fast too, right into a torn load. Heavy-duty stretch wrap for shipping should hold its stretch ratio from the first revolution to the last — that’s where quality shows.
Spotting inconsistent gauge before it reaches the dock
Gauge drift is sneaky. One roll feels fine, the next one snaps at the same tension. So check incoming cases before they hit the line.
- Pull a sample: stretch 12 inches by hand. Thin spots tear early.
- Look for ribbing: rope-like streaks mean uneven film.
- Watch the core: crushed or off-center cores cause machine jams.
- Log breaks per shift: three or more on one roll? Pull it.
Corner board, tape tie-in, and when the wrap alone isn’t enough
Film isn’t magic. Heavy, dense loads, like boxed liquids or tall stacks, need corner board to keep edges from cutting the wrap and crushing cartons.
Tie the first wraps to the pallet base, or anchor the film end with a strip of tape so it doesn’t unspool in transit. Add strapping when a load tops roughly 2,000 pounds or rides a long haul. Wrap tells you the load is held. Strapping proves it.
Buying big rolls in bulk: keeping supply steady without tying up floor space
One pallet of machine film can hold 40 rolls, and a busy line can chew through a pallet in under two weeks. That’s why a plastic wrap big roll order can’t be an afterthought. Run dry on a Friday, and you’re hand-wrapping loads with whatever’s left in the supply cage.
Case counts, storage, and par levels for a plastic wrap roll for packing
Start with burn rate. Count rolls used over four weeks, divide by four, and you’ve got a weekly number. Then set your par level.
- Reorder point: two weeks of film on the floor, plus one delivery lead time.
- Storage: keep rolls upright on their cores, off the dock, away from heat (warm film sticks and tears).
- Case counts: buy in full cases so nobody opens a box and leaves loose rolls to scuff.
Floor space is the catch. Stack too high and the bottom rolls flatten. Tight.
Handheld versus machine rolls: matching the film to the job
Handheld rolls run 15 to 20 inches wide with a light core, built for a worker walking the pallet. Machine rolls run wider, usually 30 inches, and they’re heavier. They feed a turntable or arm that controls the stretch for you, so every pallet gets the same wraps.
Here’s what most people miss: the film should match the wrapper, not the other way around. A heavy-duty stretch wrap that fits one machine can jam on another. Check core size and roll weight before you order a new case, and ask whether the gauge holds up at your stretch ratio.
Wrapping time rarely gets lost in one big way. It leaks out in thirty-second pieces, every time a short roll runs dry and a line operator walks to the rack. Multiply that across a shift and a week, and a plastic wrap big roll starts to look less like a purchasing preference and more like a labor fix.
But the roll size only pays off if the film behind it is right. Consistent gauge and a solid pre-stretch rate decide whether a pallet rides quietly to the dock or shifts on the first hard turn. Cheap film that thins out mid-roll wastes the time it was supposed to save.
The next step is simple, and it takes one afternoon. Count the roll changes on your busiest line for a single shift, then pull the gauge and core specs off the film you’re running now. Set a par level for machine rolls based on that count, and order a trial case of the heavier gauge before the next peak week hits. Run it. Time it. Let the numbers make the case.